Hey everyone, it’s Jake from the PET preform mold team here. If you’ve ever stood in front of an injection molding machine watching a preform mold cycle—like, one second the mold’s slamming shut and the next it’s flying open so fast you’re worried the ejector pins are gonna take a chunk out of something—you know that adjusting opening and closing speed isn’t just a “tweak” thing. It’s make-or-break for your preform quality, mold longevity, and even how much scrap you’re tossing at the end of a run. I’ve been dealing with this stuff for 8 years, working with brands big and small, and I still get questions weekly like, “Wait, why does my supplier’s mold run smoother than mine even though it’s the same model?” Spoiler: half the time it’s not the mold—it’s the speed settings. Let me break this down like I would to a new customer on our shop floor—no fancy jargon, just real-world fixes that work. PET Preform Mold
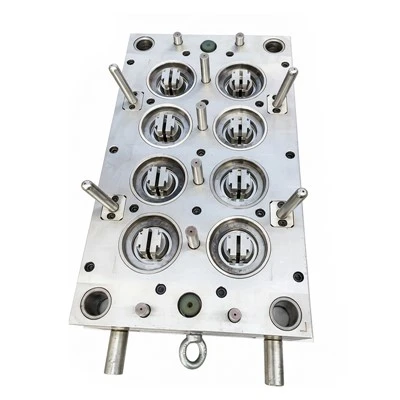
First off, let’s get one thing straight: PET preforms are tricky little beasts. They cool fast, they’re prone to flashing if you overpack, and they shrink a little more than other plastics, so if your opening/closing speed is off, you’re gonna have issues before you even inject the resin. I see so many operators just crank the speed up to max to “save cycle time” and then wonder why they get flashing on the gate, stuck preforms, or even mold halves getting dinged. That’s a rookie mistake, and I’ve fixed more than a few molds that got damaged because of overzealous speed settings.
Let’s start with closing speed, because that’s where a lot of people mess up. Closing isn’t just one single speed—it’s stages, right? If you set it to full speed the whole time, the mold halves will crash into each other, and that’s bad. I learned this the hard way early on when a new operator ran a 48-cavity mold at max close speed, and we had 6 cracked cavity inserts and a bent toggle bar. Cost me almost $2k in parts and downtime. Now, every mold we sell comes with a basic stage setting cheat sheet, but let’s talk about why the stages matter for PET specifically.
Stage 1 of closing is “approach speed”—this is when the moving platen is coming in from like 50mm away from the fixed half. This one should be fast, but not reckless. Why? We don’t wanna waste time here, but we also don’t want any side load if the platen’s a little misaligned. For most standard 24 or 48-cavity PET molds, I suggest 80-100 mm/s here. But wait—if you’re running a super small preform (like 10g for a water bottle cap liner) or a big one (like 50g for a 2L soda bottle), adjust that. Smaller molds with less mass? You can push it to 110, but bigger, heavier molds? Drop it to 70—you don’t wanna jar the mold when those heavy halves meet.
Stage 2 is “transfer speed”—this is the part where the mold halves are almost touching, like 2mm to 0.1mm gap left. This is the most critical stage for closing, especially for PET. Here’s why: PET melts at a specific viscosity, and if you close too fast here, you’re gonna get flashing—those thin, annoying bits of plastic around the edge of the preform gate. Flashing means you’re wasting resin, and it can get stuck in the mold’s vent gaps, which leads to more issues later. I usually set this transfer speed to 15-25 mm/s, but again, tweak for cavity count. More cavities mean more mass to move, so bump it up to 30 if you’re running a 72-cavity mold, but never go above 35. I had a customer with a 96-cavity mold try 40 mm/s here and they had flash on every preform—they ended up losing 12% of their scrap to that alone, and we fixed it in 10 minutes by dropping that transfer speed.
Then Stage 3 is “full close clamp”—this is where you hit the full pressure to lock the mold before injection. The speed here? Honestly, this is more about pressure than speed, but a lot of people mix them up. You don’t need to move fast here—you just need to make sure the mold is fully seated so you don’t get under-packing. If you set the speed too high here, you might overshoot and cause stress on the mold’s locking mechanism. I usually leave this at like 10 mm/s, just enough to seat, then hold clamp pressure. That’s the closing side.
Now for opening speed—this is where I see even more chaos. Operators think “faster opening = shorter cycle time = more profit” but that’s only true if you don’t have stuck preforms or damaged ejectors. PET preforms shrink as they cool, right? So if you yank the mold open too fast, the preform might not have adhered to the cavity wall enough, or wait—no, actually, if the mold opens too quick, the ejector pins might not be ready, or the preform can crack when it’s being pulled away from the core. I’ve seen a customer run a 16-cavity mold at full open speed, and half the preforms came out with a split neck because the core pulled too fast. Neck splits are a huge headache because you can’t use those preforms for blowing bottles—they leak.
Opening speed also needs stages, and for similar reasons to closing. Stage 1 of opening is “breakaway speed”—this is when the mold starts to separate from the clamped position. This should be a touch slower than the final close transfer speed, like 10-20 mm/s. Why? We wanna avoid that sudden pull on the preforms as soon as the mold starts opening. If you do it fast, you’ll get those neck splits I mentioned, or even pull the core out too quick and leave a little plastic gunk on the cavity wall, which leads to consistent defects. I had a customer who was throwing out 8% of preforms because of neck splits, and when I had him drop the breakaway speed from 35 to 15, that dropped to less than 1%—game changer.
Stage 2 of opening is “travel speed”—this is when the mold is moving open from that first gap to the ejector position, like when the halves are fully separated and the preforms are hanging on the cores. Here’s where you can crank it a bit, but again, mold mass matters. For most medium-sized molds (24-48 cavities), 50-70 mm/s works. If you’re running a small, light 12-cavity mold, you can go up to 80, but big 72-96 cavity molds? Stick to 40-50 mm/s—those moving parts are heavy, and fast speed here can cause vibration, which wears out the mold’s core pins faster. Vibration is the #1 cause of core pin wear on PET molds, by the way, so don’t sleep on that travel speed.
Stage 3 is “ejector retract speed”—wait, no, actually Stage 3 is when the mold is fully open and you’re moving toward the ejector pins. A lot of people forget the ejector part ties into opening speed. If the mold is opening too fast, the ejector pins might not activate in time to push the preforms off the cores. So that final stage of opening, just before ejector activation, should be a little slower to let the ejector system engage. I usually set that to 20-30 mm/s. If you have preforms sticking to the cores, that’s almost always because that final opening stage was too fast, so the ejector couldn’t kick in before the core pulled away.
Now, here’s a pro tip that most other mold suppliers won’t tell you: this isn’t a set-it-and-forget-it thing. You have to adjust the speeds based on a few variables that change on every run. First, resin grade. If you’re switching from standard PET resin to a recycled PET (rPET), that’s stiffer, right? So you’ll need to slow down the opening speed a little because rPET doesn’t shrink the same way as virgin PET, so it’s more likely to stick to cores. I had a customer that switched to 100% rPET and thought their mold was broken because preforms were sticking—turned out they kept the same opening speed as they used for virgin PET, and dropping the breakaway speed by 5 mm/s fixed it.
Second, mold temperature. If your mold is running hotter (I usually recommend 10-20°C for PET molds, depending on preform size), the resin cools slower, so it’s softer when you open the mold. So you can go a little faster on opening, but not by much. If the mold is too cold, the preform is hard and brittle, so even a tiny fast pull will crack the neck. I had a new customer this year who was running his mold at 5°C too cold, and his neck split rate was 15%—we bumped the mold temp 5°C and adjusted the opening speed down 3 mm/s, and that split rate went to 0.2%.
Third, cavity maintenance. If your mold has been running for a while, the cores might have a little plastic buildup, or the cavity walls are a bit worn. That changes how the preform releases. I always tell customers to check cavity release by running a test shot, then adjust the opening speed based on that. If preforms are sticking, slow down the breakaway and travel speed by 5 mm/s, not the whole opening cycle. Don’t just crank the whole thing—you’ll mess up cycle time for no reason.
Wait, let’s talk about cycle time, too, because I know everyone is obsessed with that. A lot of operators think slowing down opening/closing speed will add time to the cycle, but that’s not true if you do the stages right. The fast stages (approach and travel) are already set to be as quick as possible without causing issues. The only slow stages are the critical ones that prevent defects and mold damage. I once had a customer who thought his 48-cavity mold was running too slow, so he cranked all speeds up, ended up with broken cavities, and was down for 3 days. He lost 10k in production, and the “time he saved” by cranking speeds was 2 seconds per cycle. It would’ve taken him 2 hours to make up that 2 seconds, but 3 days to fix the mold. That’s a lesson I don’t want anyone else to learn.
Another thing: machine calibration. A lot of people blame the mold when the real issue is the injection molding machine’s pressure and speed settings not synced. We test every mold we sell on our own machine before it ships, so we send a setup guide that matches the mold to common machine models, but every shop’s machine is a little different. I always tell customers to do a “step test”: run the mold at 80% of the max closing speed, check for flashes or damage, then bump 5% until you hit the sweet spot. Same for opening speed—start low, work up until you see no sticking or splits, then leave it there.
Wait, let’s address a common question I get: can I adjust the speed directly from the machine’s HMI, or do I need to mess with the mold’s mechanical parts? For 99% of cases, you adjust it through the HMI—modern injection machines let you set each stage individually, so that’s way easier than tweaking mechanical valves. The only time you’d mess with mechanical stuff is if the machine’s stages aren’t matching up, or if the toggle bar is wearing, which would affect speed consistency. But that’s a rare thing, usually only after years of heavy use.
Let’s wrap this up with a real example, so it’s not just theory. Last month, a customer in Mexico had a 32-cavity preform mold that was producing 7% scrap from flash and neck splits. They were running the whole closing cycle at 120 mm/s and whole opening at 90 mm/s. I had them split closing into approach (90 mm/s), transfer (20 mm/s), full close (10 mm/s). Then opening: breakaway (15 mm/s), travel (60 mm/s), final opening (25 mm/s). We also had him bump the mold temp 5°C because he was running it too cold. After the tweak, his scrap rate dropped to 0.8%, and his cycle time only went up 0.5 seconds—nothing, because we just optimized the slow stages instead of slowing the whole thing down. He sent me a message 2 days later saying he made an extra $1,200 that day from less scrap. That’s the kind of win we live for.
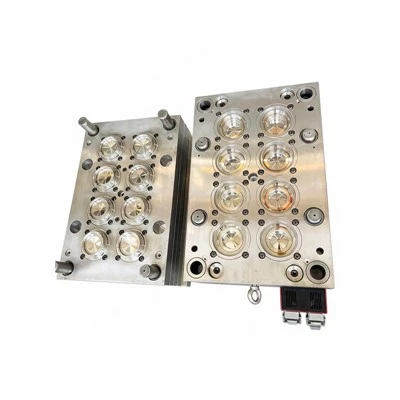
If you’re reading this and you’re still struggling with opening/closing speed, or if your mold is giving you issues with preform quality, scrap, or wear, don’t guess at it. We work with all types of shops—small operations with 1 machine, big production facilities with 50 lines. We know PET preform molds inside and out, and we can help you dial in those speed settings, or even help you source a new mold if yours is the one causing the headaches. Just reach out—we’ll walk you through it step by step, no sales pitch, just real advice from people who do this every day.
Medical Injection Mold References
- Injection Molding Handbook, Rosato, D.V., Rosato, M.G. (2000)
- PET Preform Manufacturing: Principles and Practice, Harper, C.A. (2011)
- Mold Flow Analysis for Injection Molding, Stanford University Manufacturing Extension Program (2018)
- Polymer Processing Fundamentals, University of Michigan Department of Materials Science and Engineering (2020)
Taizhou Koni Mould Co., Ltd.
As one of the most professional pet preform mold manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale high quality pet preform mold made in China here from our factory. For pricelist, contact us now.
Address: No. 97 Jinju Road, Chengjiang Subdistrict, Huangyan District, Taizhou City, Zhejiang Province
E-mail: kn@kenimould.com
WebSite: https://www.kenimouid.com/
